Bore to Side Hole
Cross holes and ports may need to relate to the central bore, OD, shoulder or end face.
 Deutsch
Turn-Mill Machining
Turn-mill machining is suitable for components that combine turned diameters, bores, flats, slots, cross holes, radial holes, threaded features, wrench faces, grooves, and multi-side details. Where possible, related features are completed in one setup to reduce accumulated error and protect datum relationships.
Turn-mill work is reviewed against the part's rotational and side features. Turning diameter up to Ø680 mm and machining length up to 1,000 mm are independent maximum limits, subject to setup and tool access.
When turned and milled features are related, moving the part between separate machines can introduce accumulated error. Turn-mill machining can reduce handling and help protect relationships between diameters, bores, flats, side holes, bolt patterns and mating faces.
One setup is not automatically required for every part. We review the drawing to decide whether the feature relationships, tolerances and quantity justify turn-mill machining.
Use turn-mill when a rotational part also needs controlled flats, cross holes, ports, slots, side threads, or bolt patterns that relate to the turned datums.
Cross holes and ports may need to relate to the central bore, OD, shoulder or end face.
Wrench flats and threaded features may need consistent angular and axial position.
Flanged components often require the central bore, bolt pattern, and sealing face to be reviewed together.
Slots, keyways and grooves may need controlled distance from a functional datum surface.
Assembly fit can depend on face quality, perpendicularity, bore condition, and burr control.
We check how related features will be measured before committing to a machining plan.
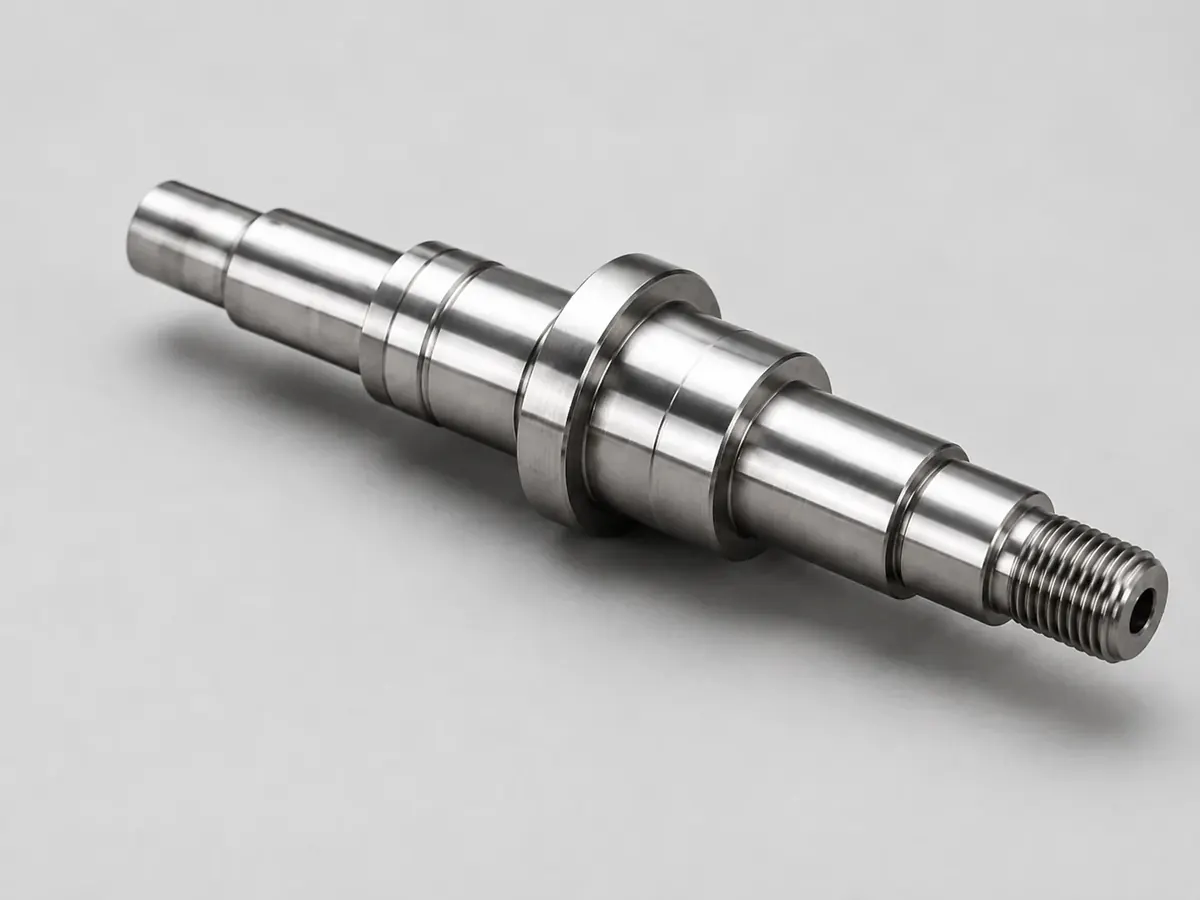
Stepped diameters, grooves, threads, shoulders, cross holes, and controlled mating surfaces.
View details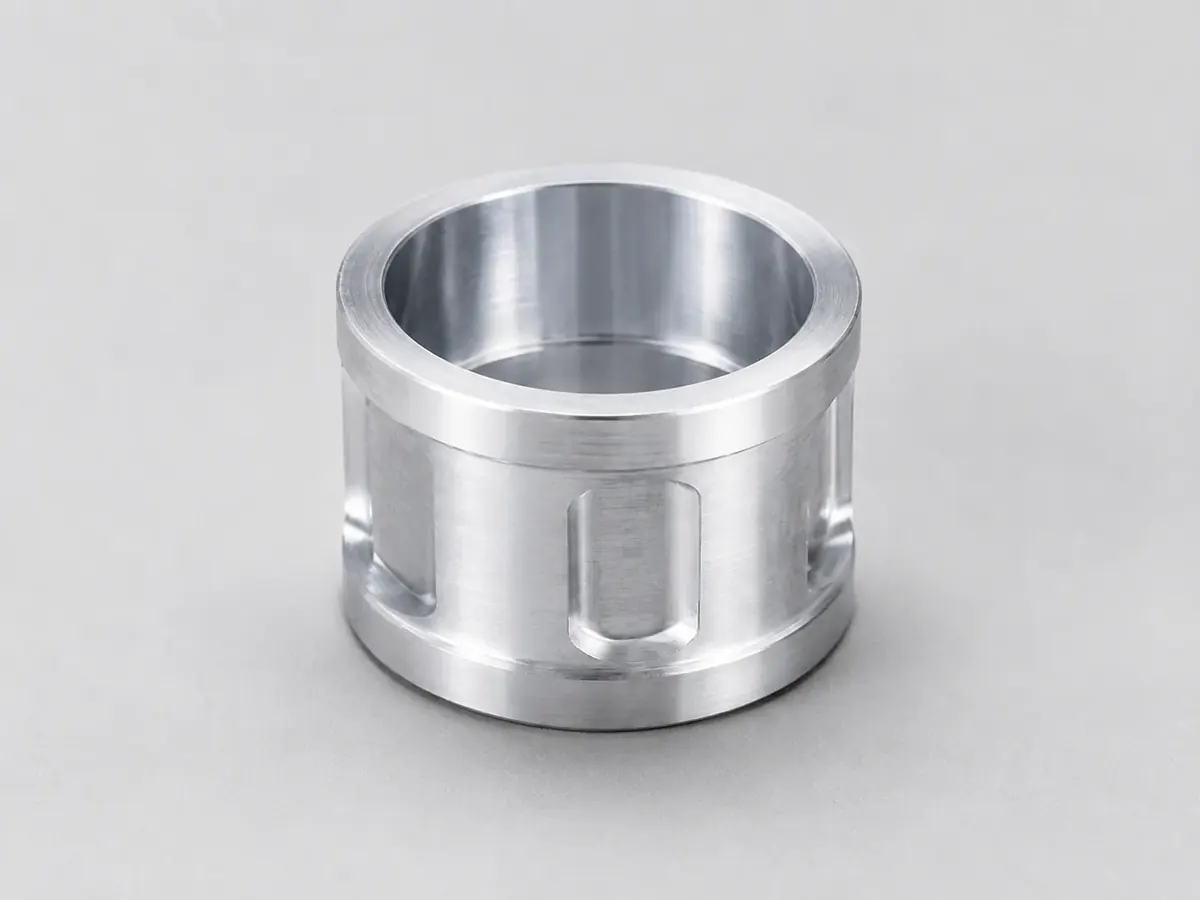
Bore control, OD/ID relationship, end-face quality, chamfering, cross holes, and deburring.
View details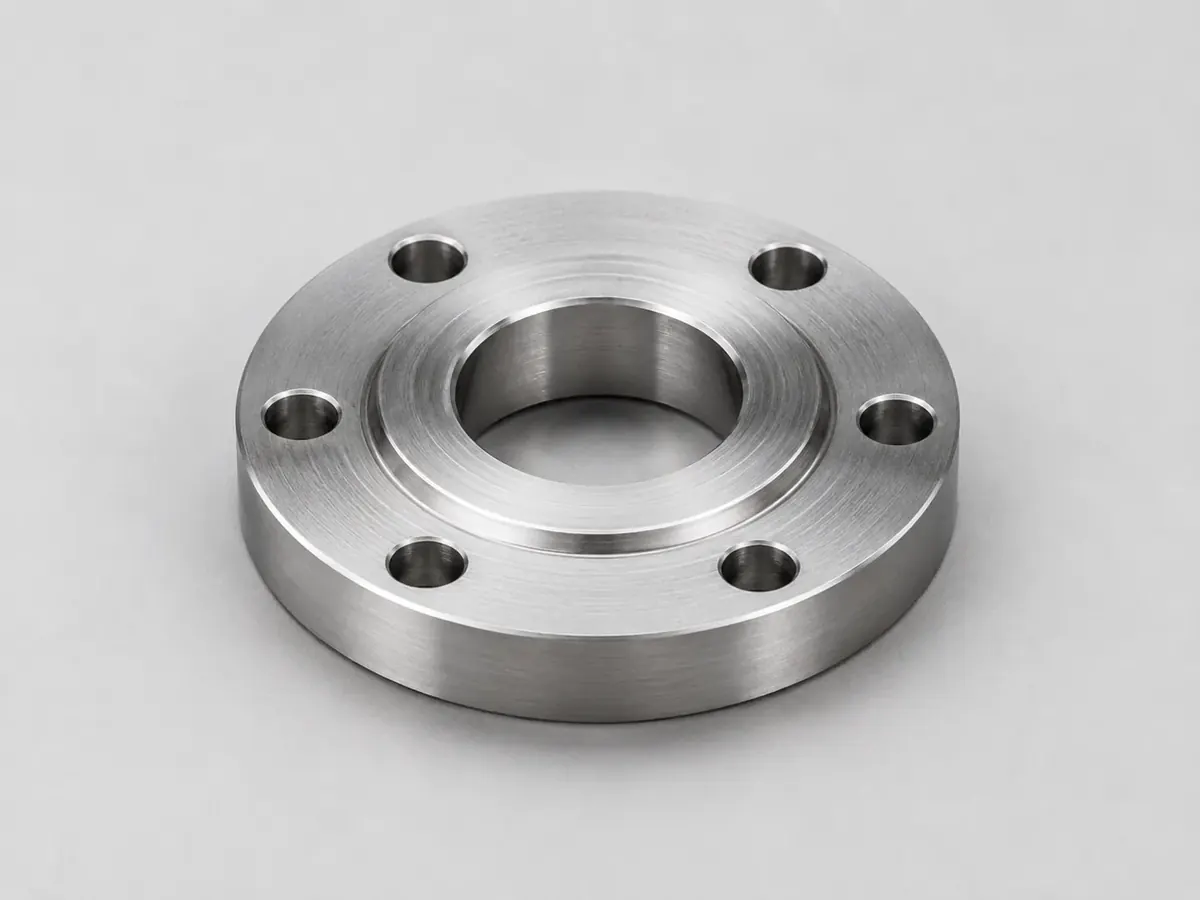
Central bores, bolt hole position, face quality, sealing surface control, and datum understanding.
View details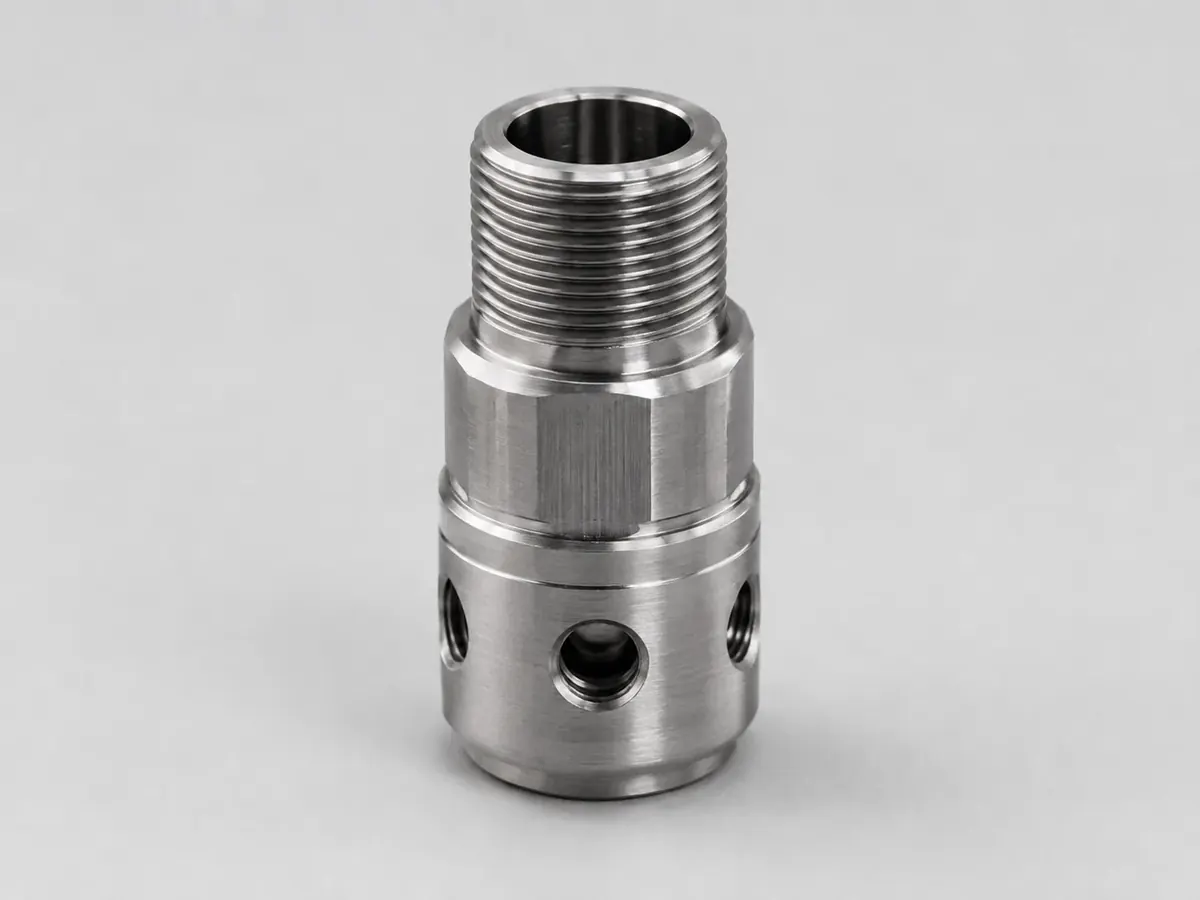
Internal and external threads, thread depth, entrance chamfer, burr control, and gauge inspection.
View detailsReview a real DXSCNC turn-mill component using customer-approved public photos. The case focuses on visible geometry, radial side-feature burr-control risk, finished-surface protection and manufacturing considerations without exposing confidential customer data.
See the real finished-part photos, evidence limits and buyer review points.
Turn-mill machining case studyReview a real DXSCNC brass turn-mill component case using customer-approved public finished-part photos. The case focuses on strict geometric tolerance review, CMM inspection planning, anti-oxidation treatment and individual packing protection.
See the public project facts, finished-part photos and buyer review points.
Brass turn-mill case studyReview a real DXSCNC production example for a 500-piece black POM long cylindrical mounting component. The page focuses on M15 end threads, milled side features, cross holes, counterbores, positional relationships and controlled plastic machining risks.
See real DXSCNC product photos and the public engineering review points for this drawing-based component.
View POM production exampleRead the engineering guide to cylindrical datums, angular positioning, cross-hole and counterbore relationships, POM workholding and inspection planning for position-sensitive turn-milled components.
The guide uses this black POM production example to separate confirmed project facts from general machining guidance.
Read feature-position guideChoose turn-mill machining when turned diameters and milled features have functional relationships or when reducing handling can reduce risk.
Yes. Cross holes, radial holes, ports and side threaded holes are common reasons to review a part for turn-mill machining.
Not always. We compare feature risk, quantity, tolerance requirements and setup complexity before recommending the process.
A 2D drawing with datum, tolerance, thread and surface finish notes plus a 3D model gives the clearest review path.
Review how side features, intersecting holes and datum relationships affect process selection and inspection planning.
Standard dimensional tolerance is ±0.01 mm. Tight tolerance down to ±0.005 mm is subject to drawing, geometry and process evaluation. Standard surface roughness is typically Ra 0.8 μm. Finer finishes, down to Ra 0.2 μm, can be evaluated for specific features depending on the machining process, grinding requirements and inspection criteria.
Projects beyond the overall machining range are individually assessed based on equipment, material, geometry and process.
See a confirmed 20,000-piece precision serrated flange ring case made directly on CNC turn-mill equipment, with natural anodizing and a central bore tolerance of ±0.02 mm.
Read the 6061 flange ring caseA real DXSCNC 316L flange demonstrates the coordinated machining of cylindrical surfaces, central threads, a circumferential hole pattern and radial connections.
View the 316L productReview a 304 stainless steel cylindrical example requiring turning, radial drilling and milled end features, with grinding considered only where the drawing requires it.
View the 304 sleeve exampleSee a black anodized 7075 component with milled windows and slots; 7050 is a separate material option.
View the 7075 aluminum product