
Aluminum for lightweight mounting flanges and covers.
Component-Specific CNC Machining
Complex Flanged & Multi-Port Components
Flanged components combine rotational machining with face, bore and mounting features. Typical parts include small flanges, flanged sleeves, valve-related connectors, mounting flanges, sensor flanges, adapter flanges and covers with a central bore or bolt pattern. These parts often need more than a simple profile cut because the bore, flange face, bolt holes and sealing surface may all relate to the same functional datum.
DXSCNC reviews flanged parts around central bore alignment, face quality, bolt-hole position, sealing face condition, thread depth, flatness where specified, and burr control around holes and edges. CNC turning is suitable for the OD, ID, bore and face features. Turn-mill machining is useful when the flange includes bolt patterns, side holes, slots, milled flats or angular features that need to stay related to turned datums.
For overseas procurement, a complete flanged-part RFQ should identify which face is functional, which bore controls alignment, whether the bolt pattern has positional tolerance, and whether any sealing surface requires special finish or protection during packing. This prevents cost and quality assumptions from being made after the order starts.
Machining Range
DXSCNC focuses on small to mid-size precision turned and turn-mill components.
Max turning diameterUp to 680 mm
Max machining lengthUp to 1000 mm
Dimensional capability: DXSCNC's ordinary dimensional tolerance is ±0.01 mm. Tighter feature requirements are evaluated for the project. Dimensions without individual tolerances follow the general tolerance standard on the customer's drawing or the project agreement.
Tolerance feasibility depends on material, geometry, part size, wall thickness, surface treatment, workholding and inspection method. Include the drawing, material requirements and quantities in your RFQ. If technical details need clarification, our team will contact you directly.
Complex Flanged & Multi-Port Component Series
DXSCNC evaluates drawing-based cylindrical housings, multi-port bodies, flanged adapters and other complex rotational components for CNC turning and turn-mill machining. This series focuses on the relationship between central bores, radial and cross-drilled holes, flange faces, bolt patterns, threads and milled features.
Image note: The nine user-supplied images below illustrate component types and possible structures. Some groups include simpler turned parts. These images are not DXSCNC production photographs, customer orders or evidence that the exact pictured parts were manufactured or delivered by DXSCNC.
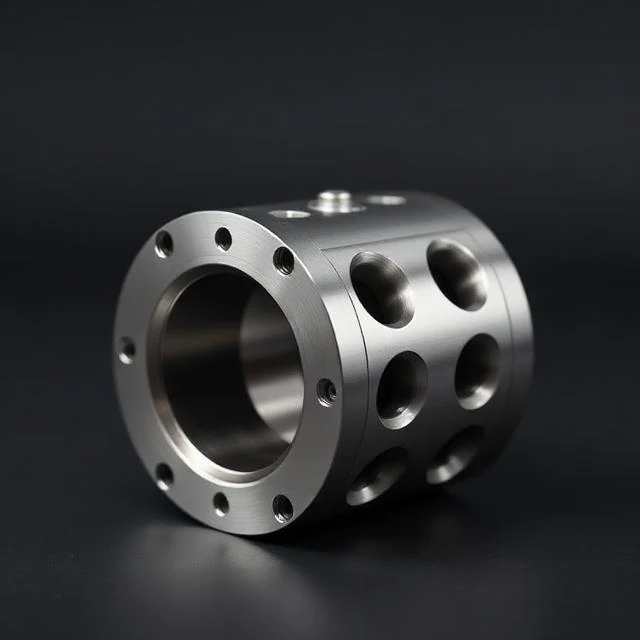
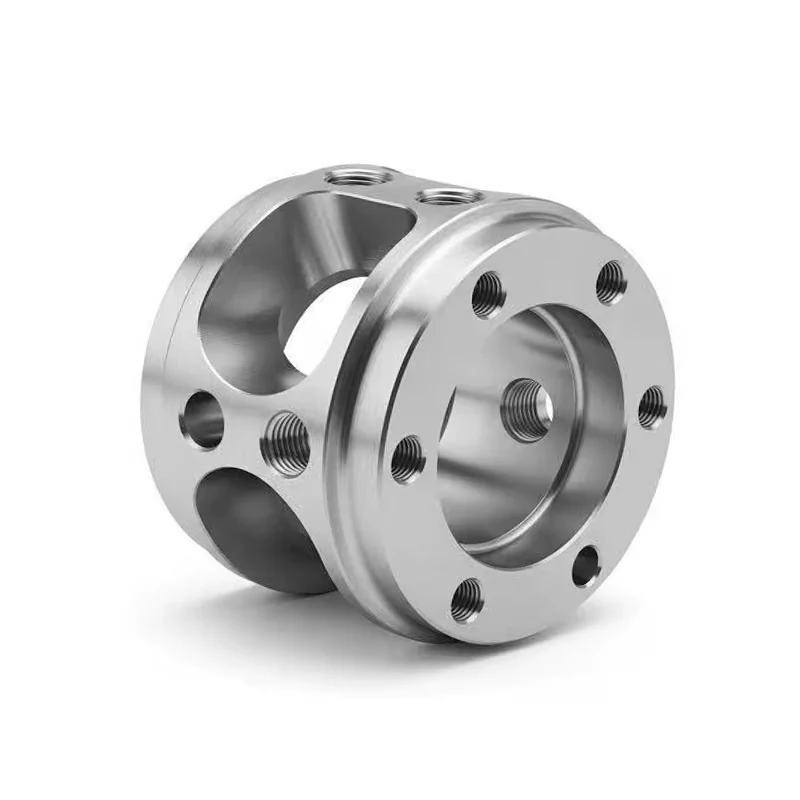
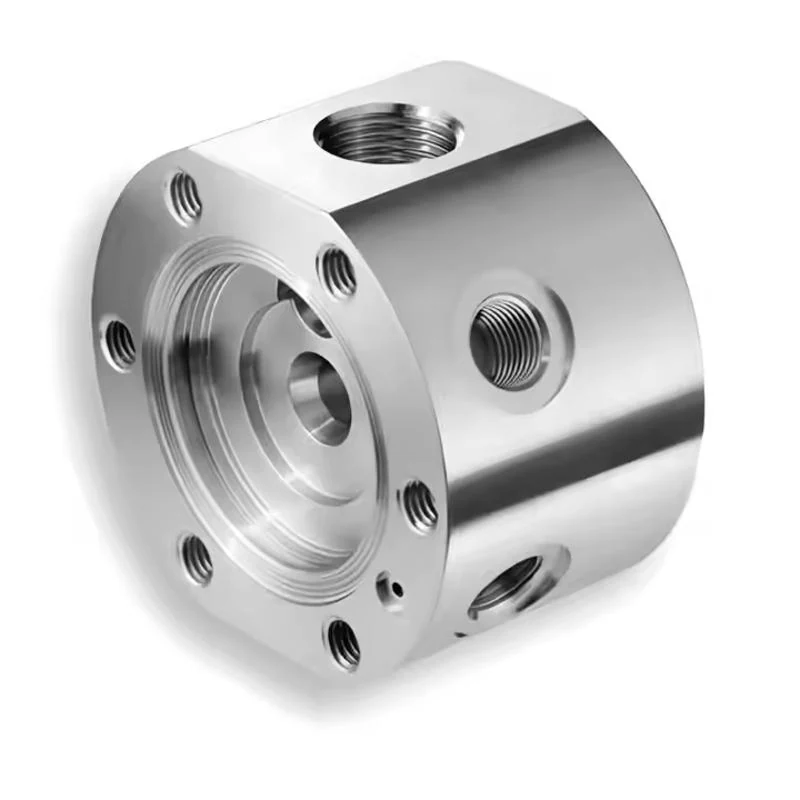
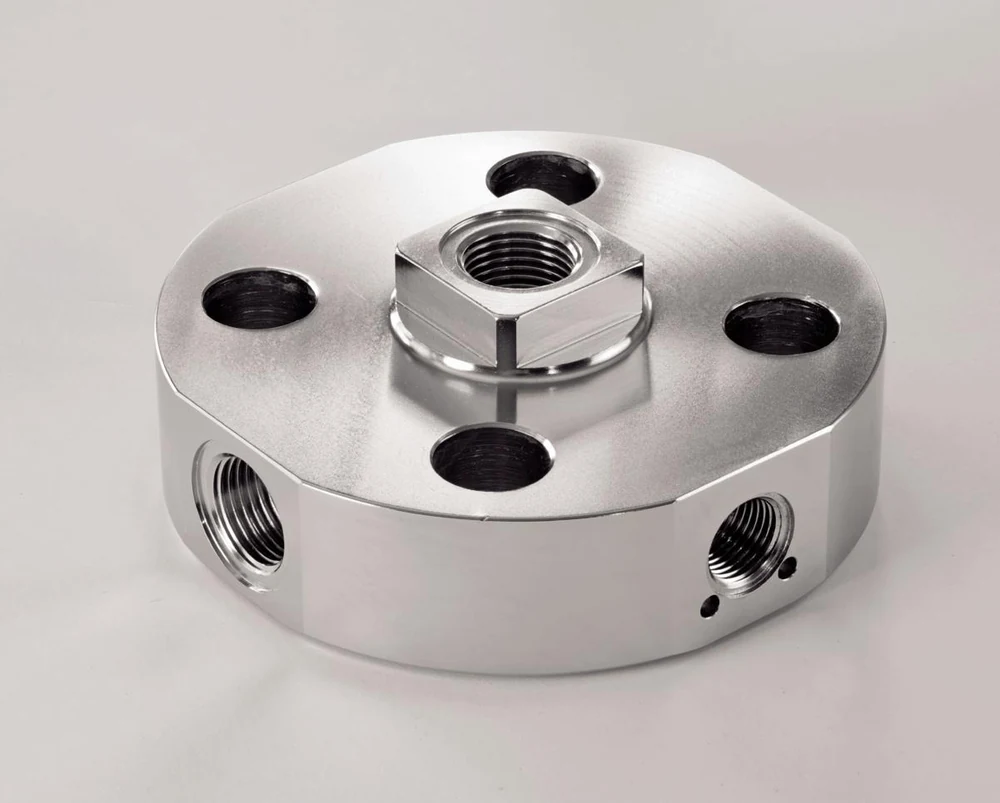
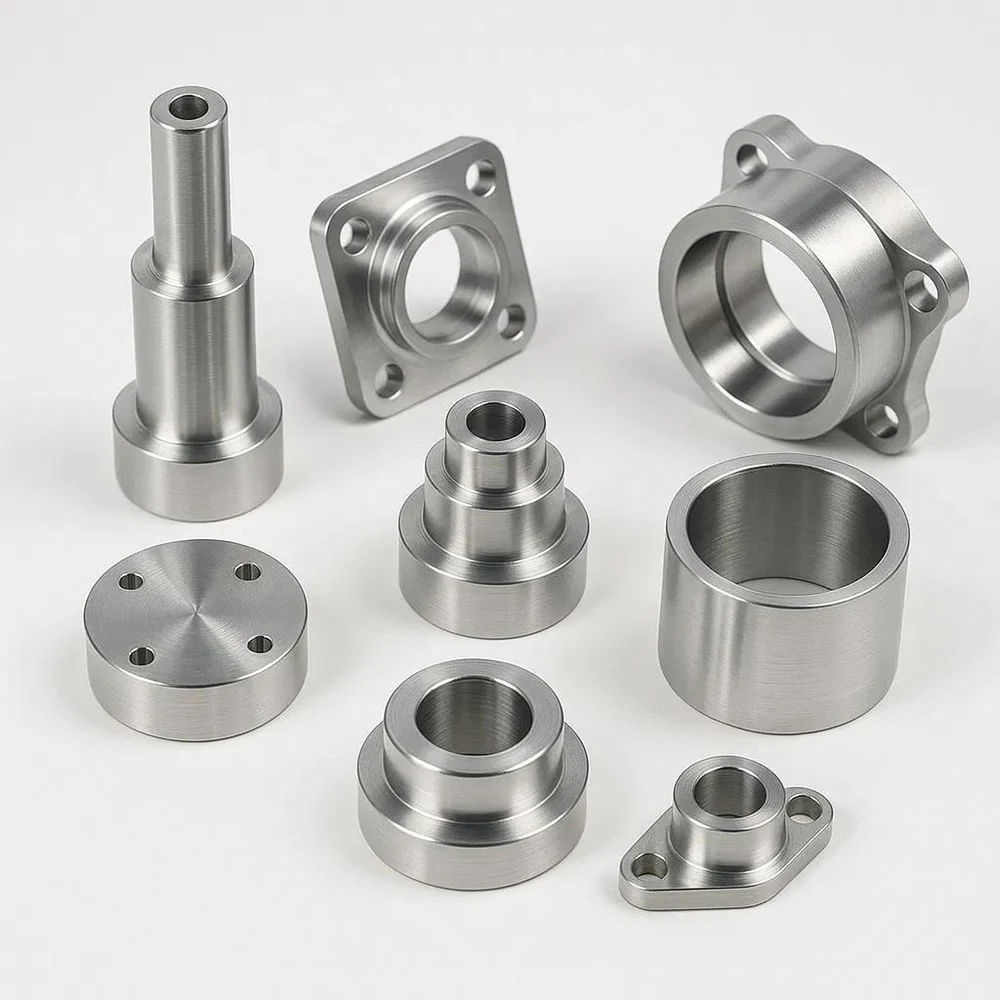
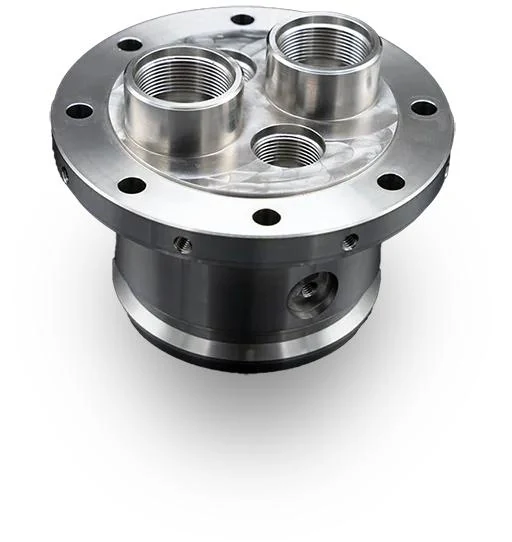
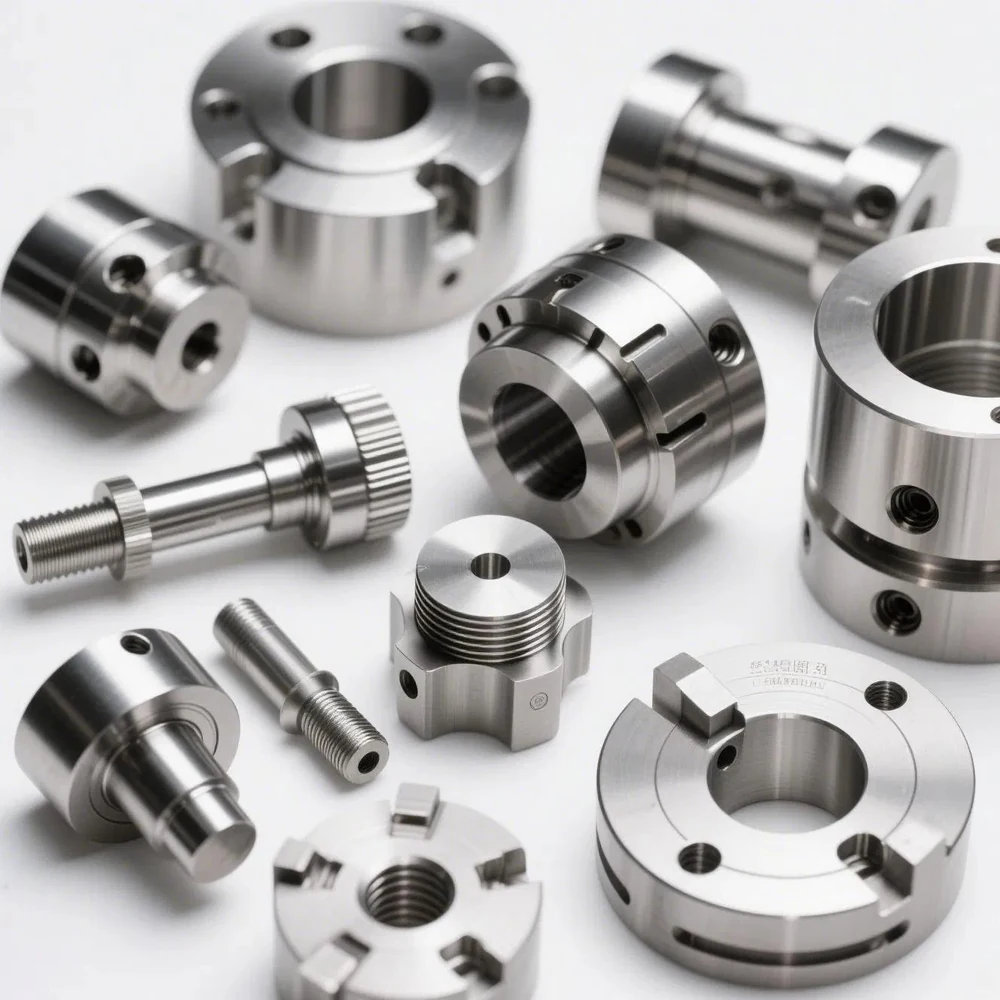
Machining features and route
Typical drawing features include precision internal bores, stepped diameters, radial and cross holes, internal or external threads, mounting faces, bolt-hole patterns, milled flats or slots, and mating or sealing surfaces. CNC turning, turn-mill machining, boring, drilling and tapping are selected according to access and datum requirements. In-house external and internal cylindrical grinding can be assessed where applicable. A single setup or machine is not assumed for every part.
Materials and inspection
Aluminum alloys, stainless steels, carbon and alloy steels, and brass or copper alloys can be evaluated against the drawing and material condition. Inspection planning may cover bore diameter, hole position, thread fit, mating faces, concentricity or runout, and surface roughness where specified. CMM inspection can be coordinated with an external provider when required; it is not implied for every order.
Explore turn-mill machining, adapters and fittings, material guidance, quality planning, and the published flanged bolt-pattern example. The case study is separate from the illustrative images above.
Typical Part Types
- Flanged sleeves
- Mounting flanges
- Valve-related flanges
- Adapter flanges
- Flanged bushings
- Covers with central bores
- Connector flanges
- Small round plates with bolt patterns
Common Materials
304 and 316 stainless steel for corrosion-resistant flanges or valve-related parts.
Carbon and alloy steel for strength or wear requirements.
Brass and copper alloys for fluid-control adapters and connector flanges.
Critical Features
- Central bores
- Bolt patterns
- Sealing faces
- Flatness or face condition where specified
- Threaded holes
- Countersinks or counterbores
- Datum relationships between bore and bolt pattern
- Chamfers and edge breaks
Manufacturing considerations
For drawing-based parts, the same nominal feature can have different manufacturing risk depending on datum references, tolerance, material, quantity and final assembly requirements.
Precision Focus
For flanged components, key precision areas may include central bore size, bolt-hole position, face flatness, sealing surface condition and bore-to-bolt-pattern relationship.
Manufacturing Risks
Risk 1
Bolt pattern position can drift if the datum relationship is unclear.
Risk 2
Sealing faces can be scratched during machining, inspection or packing.
Risk 3
Thin flanges may distort from clamping or material removal.
Risk 4
Threaded holes and cross features require burr control.
Risk 5
Surface treatment can affect sealing faces or threaded holes if masking or allowance is not reviewed.
Inspection Focus
- Bore size and bore position
- Bolt pattern and hole diameter checks
- Face thickness and flatness when specified
- Thread checks
- Sealing face visual review
- Burr checks around holes and chamfers
Surface Treatment Considerations
Flanged parts may require anodizing, plating, passivation, black oxide, polishing or protected bare machined faces. Buyers should indicate if sealing faces must remain untreated, masked or protected during finishing and export packing.
Surface treatment can affect final dimensions, thread fit, cosmetic appearance, corrosion resistance and packing requirements. Please identify surfaces that must remain protected, masked, untreated or measured after finishing.
Finishing notes to provide
- Anodizing, plating, passivation, black oxide or other finish
- Color or appearance requirement if relevant
- Masking requirement for bores, threads or sealing faces
- Dimensions required before or after treatment
- Packing sensitivity for finished surfaces
Project details to include
- 2D drawing and/or 3D model
- Material grade and equivalent standard
- Quantity and expected repeat demand
- Surface treatment or heat treatment
- Critical tolerances and datum references
- Thread standard, fit and depth
- Surface finish requirements
- Burr-free or sealing-face areas
- Application or assembly notes
- Target delivery date
Request a quotation for your part
Request a QuoteRelated Capabilities
Related Materials
Related Applications
Related Brass Turn-Mill Case
Review a real DXSCNC brass turn-mill component case using customer-approved public finished-part photos. The case focuses on strict geometric tolerance review, CMM inspection planning, anti-oxidation treatment and individual packing protection.
Brass turn-mill component with CMM inspection
See the public project facts, finished-part photos and buyer review points.
Brass turn-mill case studyRelated Q345R Pressure Component Production Example
Review a DXSCNC-owned Q345R sealed gas-chamber component production example. The public page focuses on CNC turning, sealing-related features, nickel-plating allowance, dimensional review and inspection planning without publishing customer or drawing information.
Q345R nickel-plated pressure component
The supplied project requirement identifies gas service up to 6 MPa; the page does not present a public pressure-test record or product certification.
View production exampleFAQ
Can DXSCNC machine flanges with bolt patterns?
Yes. Bolt patterns are reviewed as turn-mill or secondary milling features related to the central bore and face datums.
What sealing face notes are useful?
Provide surface finish, flatness if required, coating restrictions and packing sensitivity for sealing surfaces.
Can flanged components include threaded holes?
Yes. Please provide thread standard, depth, fit and burr-free requirements for threaded holes.
How are flanged parts packed?
Packing depends on the drawing, but sealing faces, threads and cosmetic surfaces can be individually protected when required.
Related Flanged Component Example
Review how the central bore, flange face and bolt pattern should be controlled from a clear datum scheme.
Real 6061 serrated flange ring production case
A separate DXSCNC production case documents 20,000 independent 6061 aluminum flange rings made by integrated CNC turn-mill machining. Its four photos are real production evidence; the nine product-series reference images above are illustrative.
Read the real 6061 flange ring caseReal 316L multi-port flanged component
Explore a DXSCNC-manufactured 316L cylindrical flange with three central threaded ports, circumferential holes and a radial side connection. Four actual product photographs document the part; dimensions and tolerances are not published.
View the 316L product