6061 aluminum machining
Material and temper considerations for a new drawing.
View material guide
Real Manufacturing Case Study
A 20,000-piece 6061 aluminum production batch made on CNC turn-mill equipment, with natural anodizing and a central bore tolerance of ±0.02 mm.
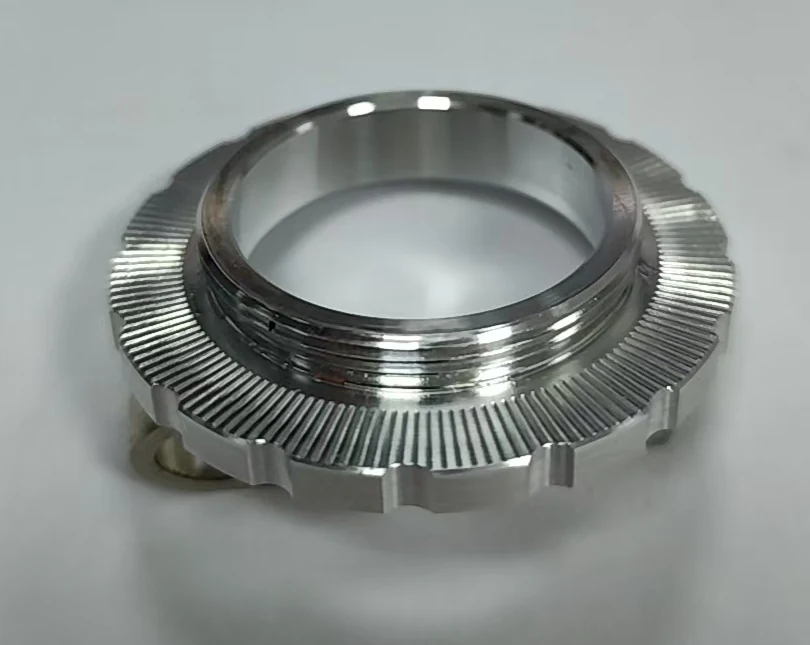
The ±0.02 mm value applies to the central bore only; it is not a general tolerance for every feature.
These four DXSCNC-supplied photographs show the independent flange ring from different views. No customer drawing, private dimensions or inspection report is published.
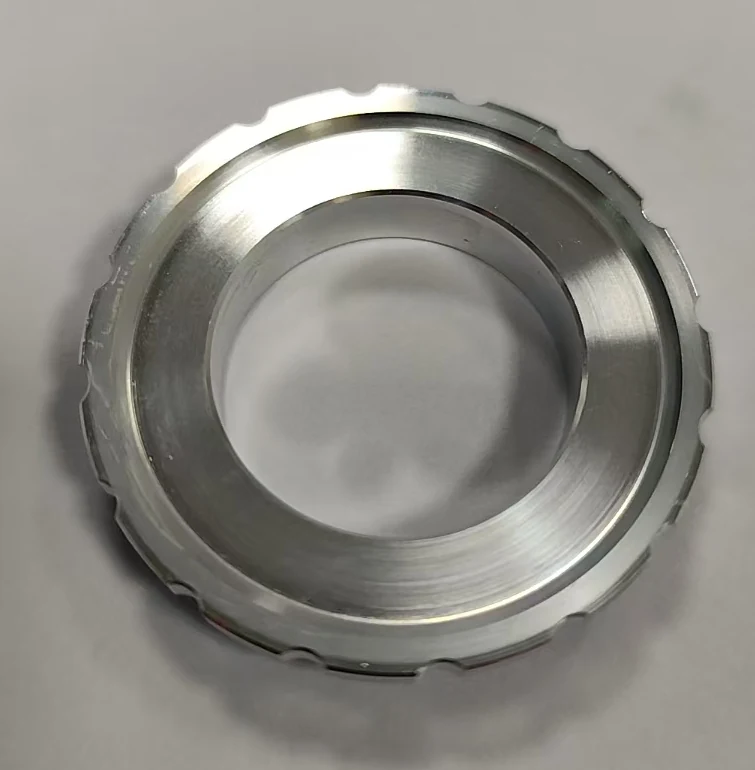
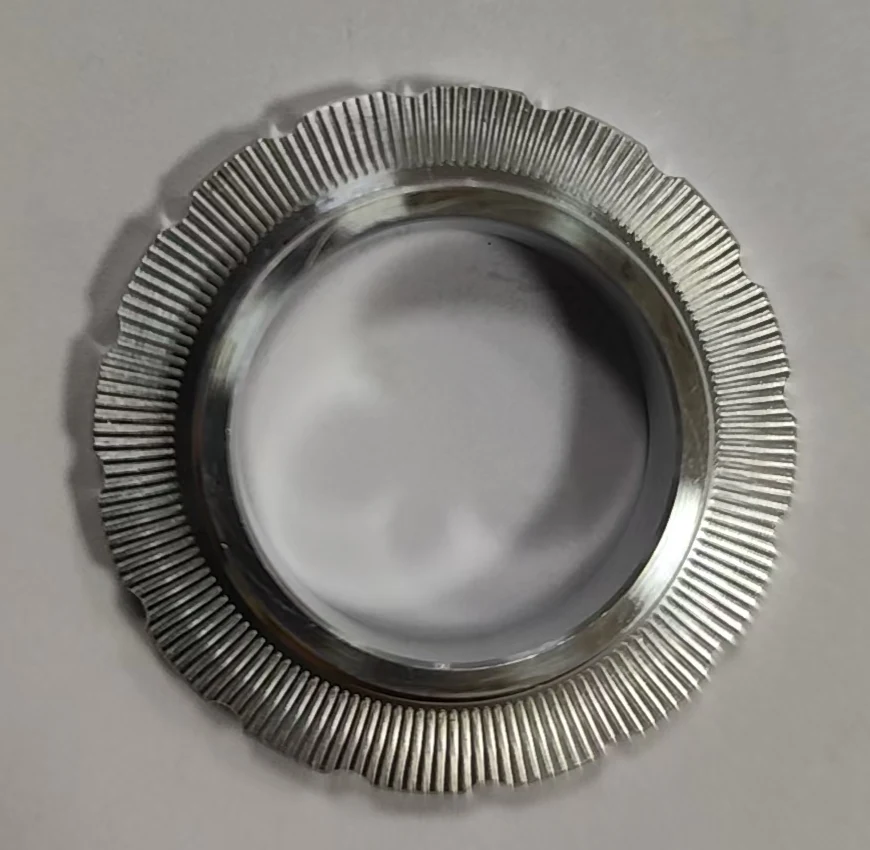
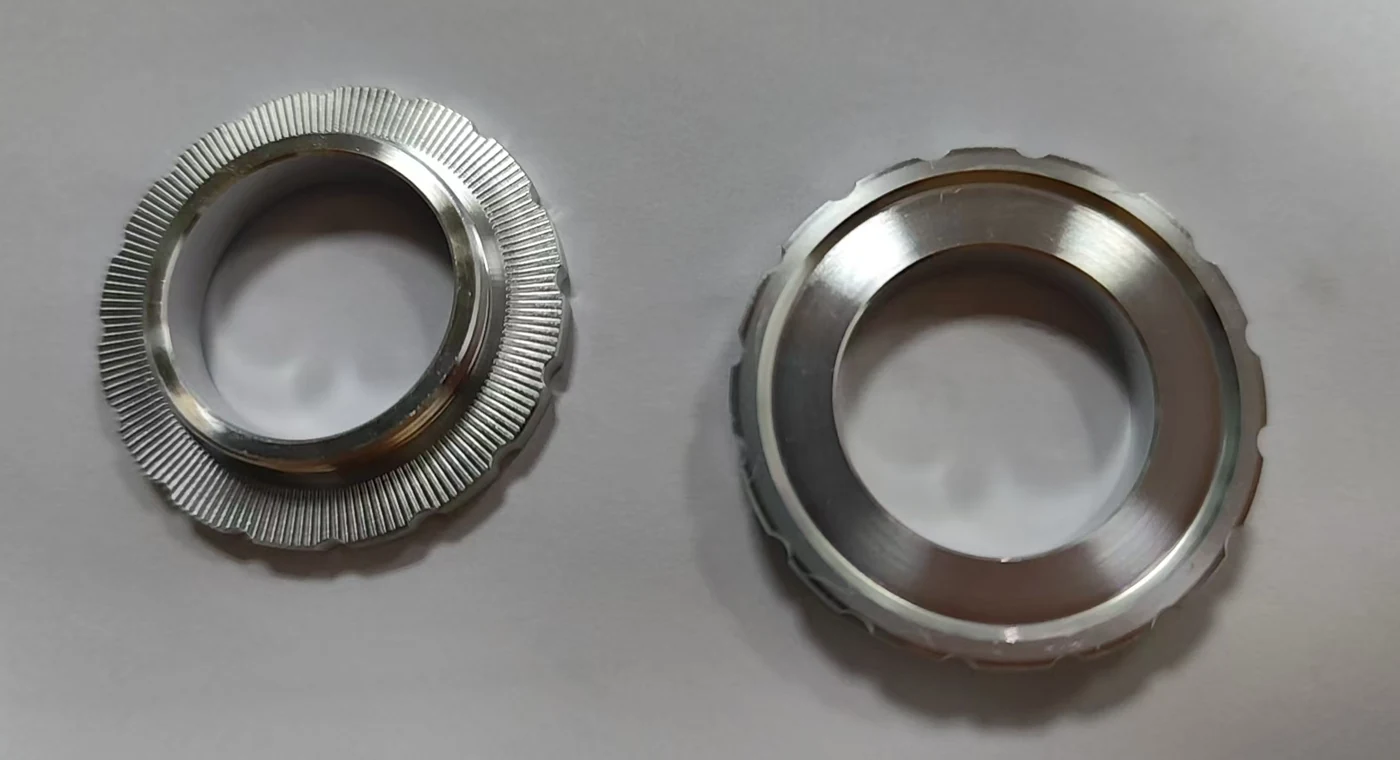
DXSCNC produced 20,000 independent precision flange rings from 6061 aluminum alloy. The component combines a central bore, stepped circular geometry, a flange profile, a fine machined serrated face and outer perimeter features. It is a single part, not a matching lock-ring set.
The turning and additional machined features were completed directly on CNC turn-mill equipment as one integrated manufacturing route. The serrated face was machined as part of that route; this case does not claim a separate gear-cutting, knurling or independent milling process. The central bore requirement and feature relationships guided part-specific machining and dimensional control.
Natural anodizing was applied to the 6061 aluminum components. The finish and central bore requirement were considered together during manufacturing. The confirmed 20,000-piece batch demonstrates DXSCNC's experience with repeated production of this precision aluminum turn-mill part; no unpublished inspection values or delivery claims are implied.
Material and temper considerations for a new drawing.
View material guideReview bore, flange face and mounting-feature relationships.
View component seriesLearn when combined turned and milled features need a coordinated route.
View capabilityDefine inspection requirements against your own drawing.
View quality planningDXSCNC manufactures custom precision CNC turned and turn-mill components in aluminum alloys, stainless steels, carbon and alloy steels, brass and engineering plastics. Typical dimensional tolerances are around ±0.01 mm for suitable features. Selected critical dimensions can be evaluated down to ±0.005 mm according to geometry, material, workholding, process and inspection requirements. This is a project-specific review, not a blanket guarantee.
Prototype quantities, small batches and repeat production orders can be reviewed according to project requirements. Send a 2D drawing or 3D CAD model, material condition, quantity and critical dimensions for technical review and quotation.
For 6061 flange rings, confirm temper and stock form, anodizing thickness and masking, the final bore size after coating, the serrated-face requirement and batch consistency criteria. The published 20,000-piece ring is a documented project; its center-bore ±0.02 mm requirement applies only to that case.
Aluminum alloy machining guide · CNC capabilities · Inspection and quality · Send drawings for a quote
Send your 2D drawing or 3D model with material condition, quantity, central bore and other critical tolerances, serration requirements, finish specification and inspection needs. Your part will be reviewed on its own requirements.
Send your drawings